Lawn Care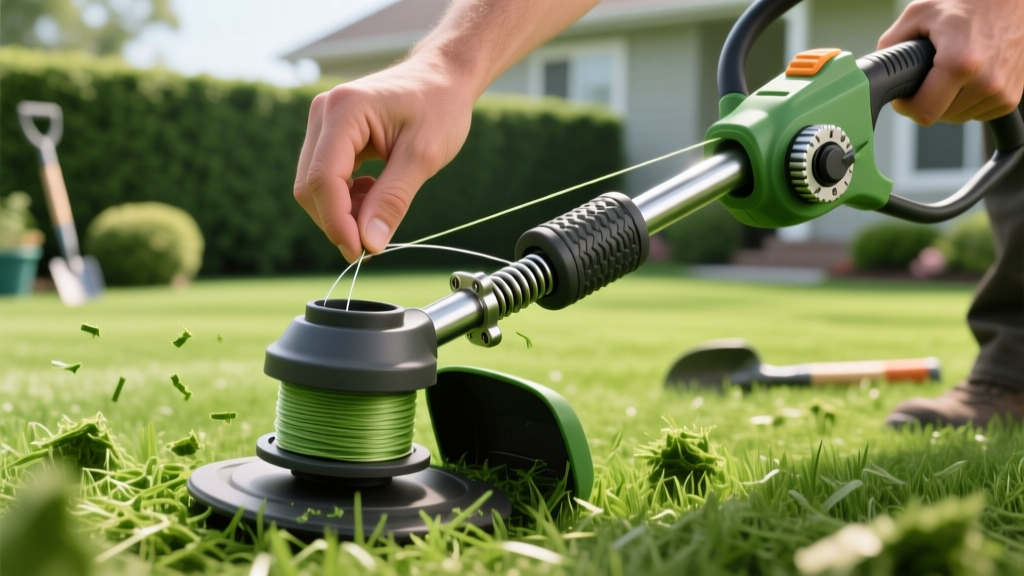
How to Load String Trimmer Line: Bump Feed & Fixed Head Guide
The Physics of Trimmer Line Failure
Most string trimmer failures occur not because the line is old, but because it was loaded with incorrect tension or wound in the wrong direction. When professionals evaluate how to load string trimmer spools correctly, they are fundamentally managing friction and kinetic energy. Inside a bump-feed head spinning at 7,500 RPM, centrifugal force pulls the line outward. If the line is wound loosely on the inner spool, the outer layers bite into the inner layers under load. This creates immense friction, generating enough heat to melt standard nylon lines together into a solid, fused block—a failure mode known as friction welding.
Furthermore, overlapping winds cause the line to bind in the spool chamber, preventing the bump-feed mechanism from advancing new line. According to the CDC NIOSH Landscaping Safety Guidelines, equipment failure and debris kickback from improperly maintained trimmers account for a significant percentage of landscaping eye and leg injuries. Mastering the loading process for your specific head type is the first line of defense against both mechanical downtime and physical injury.
Matching Line Diameter and Geometry to Your Engine
Before loading, you must select the correct line. Using a 0.095-inch line on a 21cc residential trimmer will overload the clutch and stall the engine, while using 0.065-inch line on a 40cc commercial brushcutter will result in instant snapping and excessive eyelet wear. Line geometry also dictates cutting efficiency and noise levels.
| Line Diameter | Engine Size (CC) | Primary Application | Recommended Material |
|---|---|---|---|
| 0.065" - 0.080" | 15cc - 25cc | Light residential edging, soft weeds | Standard Nylon |
| 0.085" - 0.095" | 26cc - 32cc | Prosumer, thick grass, light brush | Copolymer Blend |
| 0.105" - 0.130" | 33cc - 42cc | Commercial daily use, heavy weeds | Copolymer / Titanium |
| 0.145" - 0.155" | 43cc - 55cc+ | Brushcutting, woody stems, saplings | Reinforced Copolymer |
Line Shape Profiles
- Round: The standard profile. It bends easily and feeds smoothly through eyelets but lacks a cutting edge, relying purely on kinetic impact to tear grass.
- Multi-Sided (Square/Star): Features sharp edges that slice through thick stalks cleanly. However, the sharp corners increase drag and can melt faster in high-friction spools.
- Twisted: The twisted profile reduces aerodynamic drag, lowering noise levels by up to 20% and increasing RPM efficiency. Ideal for noise-restricted commercial zones.
How to Load a Standard Bump-Feed Spool
Standard dual-line bump-feed heads, such as the Husqvarna Tap n Go T25 or the OEM spools on Echo SRM-225 models, require complete disassembly and manual winding. The most common mistake here is ignoring the directional arrows molded into the spool housing.
- Disassemble and Clean: Press the side tabs or unscrew the center bump knob (note: many bump knobs use reverse/left-hand threads). Remove the spool and wipe out accumulated grass clippings and dirt from the inner hub. Debris inside the hub prevents the spool from dropping down to engage the bump mechanism.
- Anchor the Line: Cut two equal lengths of line (typically 15 to 20 feet each). Locate the center anchor hole on the spool. Fold one piece of line in half to form a loop, and insert the loop into the anchor slot. Pull the two free ends through the loop and cinch it tight against the center hub.
- Wind Under Tension: Locate the directional arrows on the top of the spool. Wind the line tightly in the direction of the arrows. Crucial Step: Maintain heavy, manual tension on the line as you wind. The line should feel as tight as a guitar string. Loose winding guarantees friction welding later.
- Secure the Ends: Once you reach the last 6 inches of line, snap the ends into the temporary retention notches on the spool rim. Thread the free ends through the metal exit eyelets on the outer housing.
- Reassemble and Test: Align the spool over the drive splines, pull the line ends to release them from the retention notches, and screw the bump knob back on. Pull the lines sharply to ensure they advance and lock into the cutting position.
Pro Tip: If your trimmer head lacks a center anchor hole, look for a small slit on the inner rim of the spool. Bend the first inch of the trimmer line at a 90-degree angle, wedge it into the slit, and begin winding.
Loading Speed-Feed and Quick-Load Heads
Modern commercial heads like the Echo Speed-Feed 400 or the Stihl AutoCut EasySpool 30-2 eliminate the need to remove the spool entirely. These heads are designed for rapid reloading in the field, cutting downtime from 5 minutes to roughly 30 seconds.
- Align the Arrows: Rotate the outer spool housing by hand until the alignment arrows on the top of the bump head match the arrows on the side eyelets. You will feel a distinct click when the internal channels align perfectly.
- Feed the Line: Take a single, continuous length of precut line (usually 18 to 24 feet, depending on the manufacturer's spec). Insert one end into the left eyelet and push it through the internal channel until it protrudes from the right eyelet.
- Center and Pull: Grab both ends and pull them equally until you have an equal length of line extending from both sides of the head.
- Wind the Spool: Rotate the outer winding knob (usually located on the top or side of the head) in the direction of the molded arrows. The internal mechanism will automatically grab the line and spool it under factory-perfect tension. Stop winding when about 6 inches of line remain exposed on each side.
Fixed-Line Head Loading for Commercial Brushcutters
For heavy-duty clearing tasks involving woody brush and saplings, professionals use fixed-line heads (often called metal blade heads or loop heads). These do not use a spool; instead, they hold short, precut lengths of heavy 0.130" to 0.155" line in a metal retaining plate.
- Cut to Length: Cut 4 to 6 pieces of heavy copolymer line to the exact length specified by the head manufacturer (usually 12 to 14 inches).
- Fold and Insert: Fold each piece in half to create a U-shape. Insert the folded loop into the designated slot on the metal retaining plate.
- Lock the Line: Pull the two free ends through the locking channel. The centrifugal force during operation will pull the loop tight against the inner retaining pin, securing it without the need for knots or tools.
- Inspect the Thrust Washer: Before reattaching the head to the gearbox, inspect the Teflon or bronze thrust washer. If it is grooved or cracked, replace it immediately to prevent gearbox seizure.
Troubleshooting Common Loading Errors
Even with perfect technique, environmental factors and worn components can cause feed issues. Use this diagnostic matrix to resolve persistent problems.
| Symptom | Root Cause | Corrective Action |
|---|---|---|
| Line will not advance when bumped | Dirt in hub or worn bump spring | Disassemble, wash hub with degreaser, replace spring if compressed. |
| Line breaks flush at the eyelet | Eyelet wear or incorrect line shape | Inspect metal eyelet for sharp burrs; file smooth or replace housing. Switch from square to round line. |
| Line feeds too much and tangles | Worn spool cam or dirty retention teeth | Clean the plastic cam teeth on the spool base; replace spool if teeth are rounded off. |
| Spool cracks near the center hub | Over-tightening the bump knob | Hand-tighten the bump knob only. Do not use pliers or wrenches on plastic knobs. |
Safety Warning: Never substitute commercial trimmer line with wire, metal cable, or fishing line. The OSHA Worker Safety in Landscaping guidelines explicitly warn against unauthorized modifications to cutting heads. Metal wire can shear off at 7,500 RPM, turning into lethal projectiles that will easily penetrate standard ANSI-approved safety chaps and face shields. Always use EPA-compliant, manufacturer-rated monofilament lines designed to shatter upon impact with hard surfaces.
Properly loading your string trimmer is a mechanical discipline that directly impacts your equipment's lifespan and your safety. By matching the correct copolymer diameter to your engine's CC rating, maintaining strict winding tension, and keeping the inner hub free of organic debris, you will eliminate friction welding and ensure consistent, uninterrupted cutting performance throughout the entire mowing season. For further details on maintaining the 2-cycle engines that power these heads, consult the EPA Small Engine Maintenance Guidelines to ensure your fuel mixture and air filters are optimized for high-RPM trimming tasks.